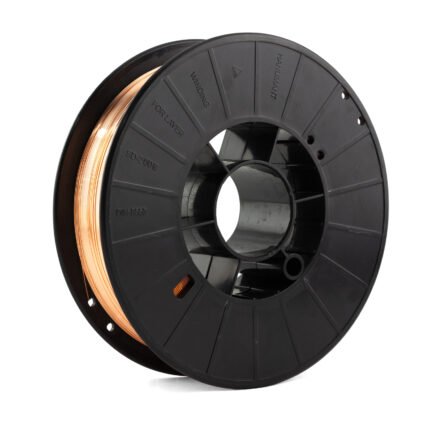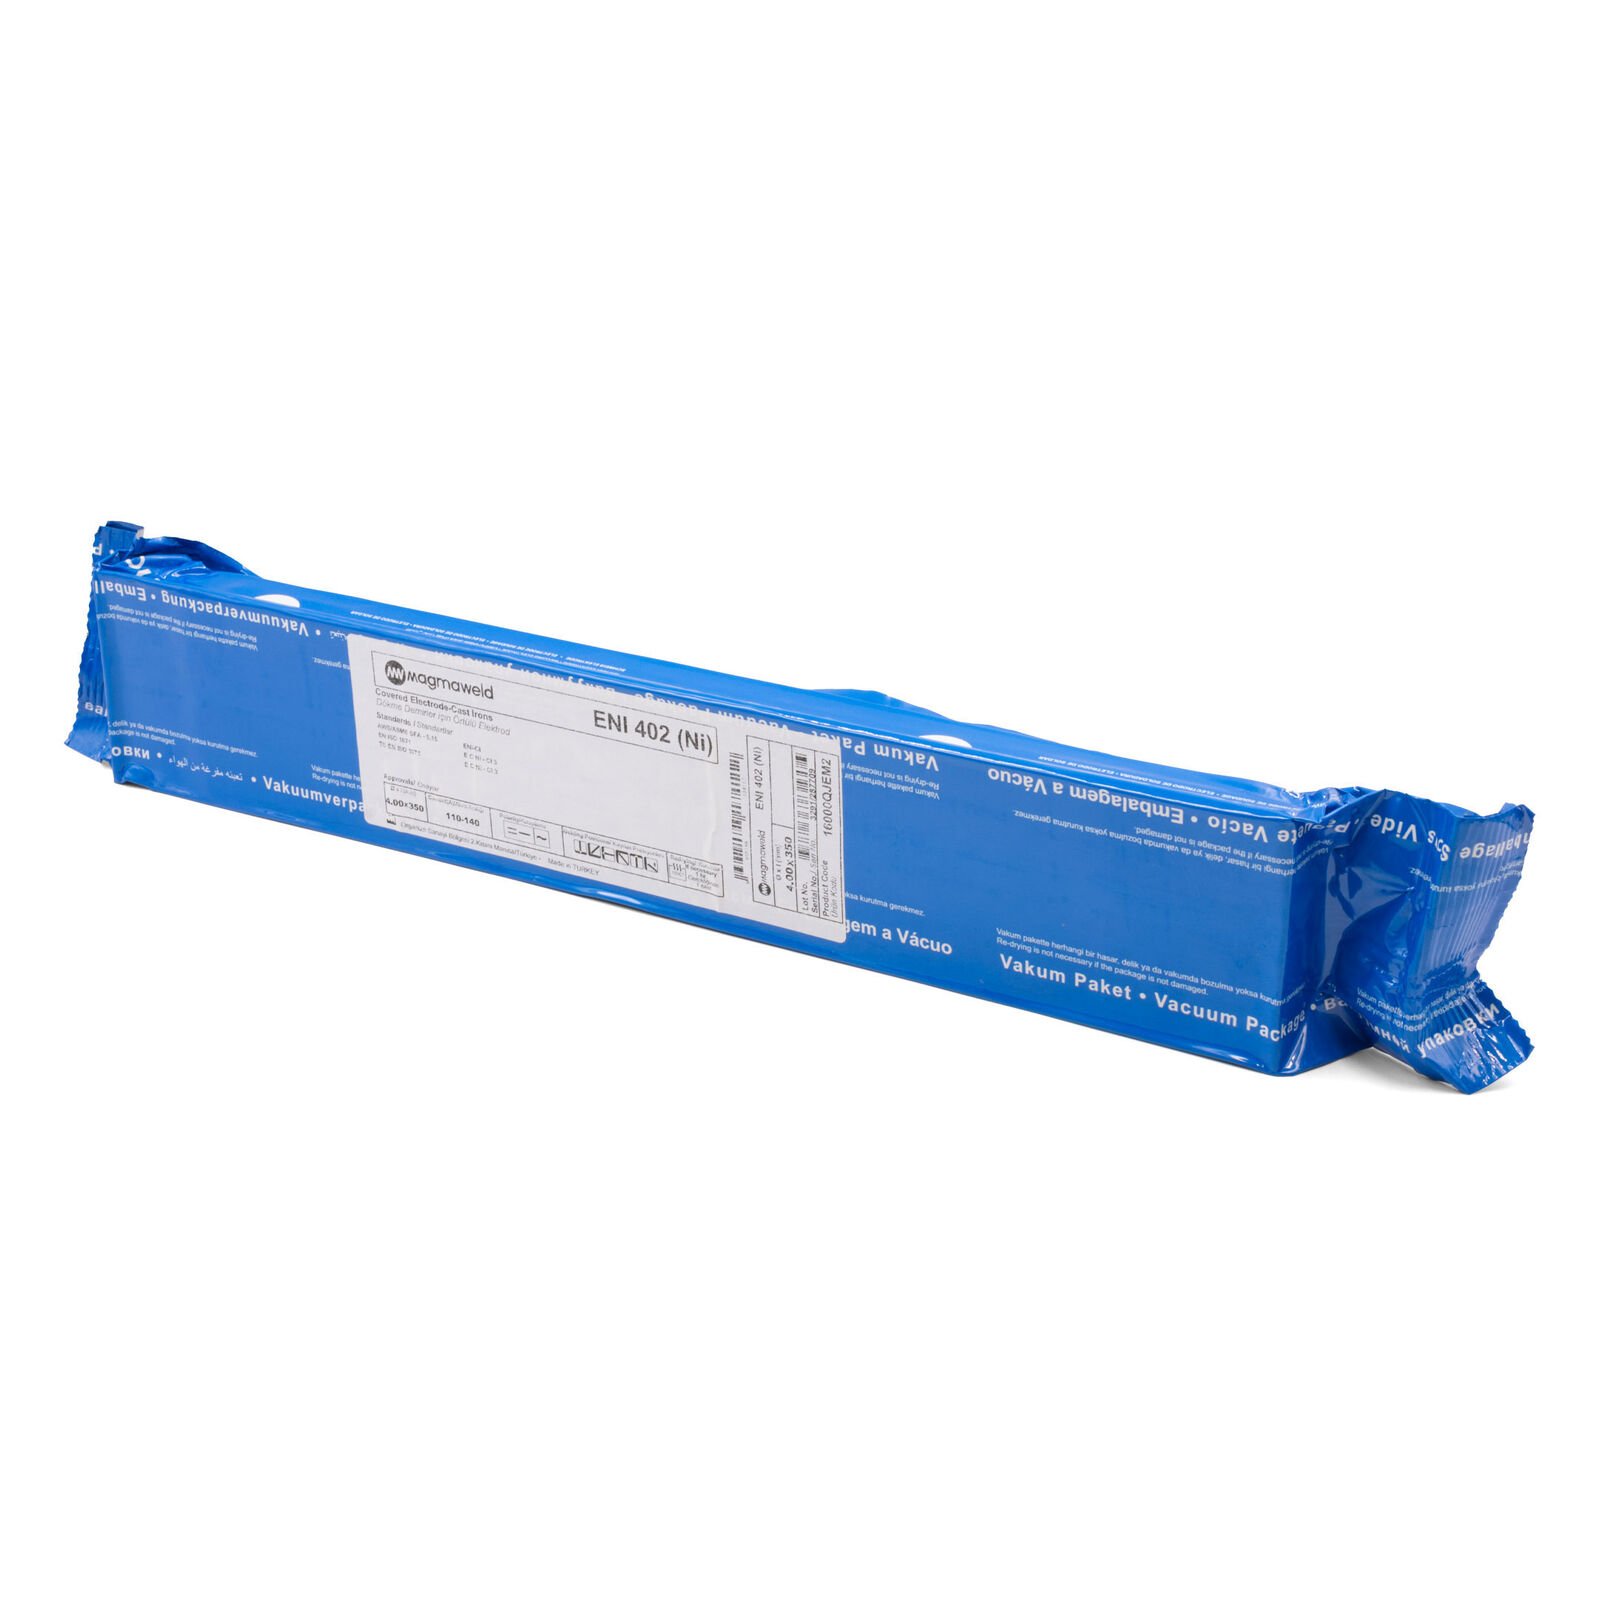




MAGMAWELD ENi99 4.0mm Cast Iron Nickel Stick Electrodes 10KG
$1,399.00
Product Description
Magmaweld ENi99 is a premium 99% Nickel cast iron stick electrode, ideal for low/medium phosphorous cast iron repairs. Features easy arc striking, stable arc, and machinable weld metal. Suitable for joining steel, copper, or nickel to cast iron with minimal preheating (max. 300¡ãC).
Specifications
| Diameter | 4.0mm |
| Length | 400mm |
| Weight | 10kg (¡Ö200 sticks) |
| Nickel Content | 99% |
| Standards | AWS SFA-5.15, EN ISO 1071 |
MAGMAWELD ENi99 – Premium Cast Iron Nickel Welding Electrodes 4.0mm 10KG Pack
Core Specifications
| Nickel Content | 99% |
| Diameter | 4.0mm |
| Length | 400mm |
| Weight | 10kg |
| Quantity | Approx. 200 sticks |
| Standards | AWS/ASME SFA-5.15, EN ISO 1071 |
| Hardness (As Welded) | 160 HB |
| Storage | Max 5 re-dries at 350¡ãC for 2 hours |
| Welding Position | PA, PB, PC, PD, PE, PF |
| Polarity | DCEP (preferred), AC compatible |
Why Choose ENi99 Electrodes?
Engineered for industrial-grade cast iron repairs, these 99% nickel electrodes deliver exceptional strength for critical applications. The pure nickel core ensures superior crack resistance and machinability, ideal for low/medium phosphorous castings. Experience stable arc performance, smooth bead formation, and minimal spatter with Magmaweld’s market-leading technology.
Applications & Performance
Perfect for welding lamellar graphite, malleable, and nodular cast iron. Ideal for repairing cracked components or joining cast iron to steel/copper. Weld metal maintains 160 HB hardness and allows single-pass repairs. Recommended preheating up to 300¡ãC for optimal results.
Quality Assurance
Manufactured in Turkey to international standards (AWS/EN ISO). Each 10kg pack undergoes rigorous testing to ensure consistent chemical composition (97.5% Ni, 0.40% C) and mechanical performance. Industrial-grade packaging ensures electrode integrity during storage.
FAQ
Q: Can these electrodes be machined after welding?
A: Yes, the weld metal is machinable with proper technique.
Q: What’s the recommended welding current?
A: Consult your welding machine manual for 4.0mm electrode settings.
Q: How to store unused electrodes?
A: Keep in dry conditions; re-dry at 350¡ãC for 2 hours if exposed to moisture.
Ready to enhance your cast iron welding projects? Contact us today for bulk pricing and technical support!